1. Scope
MSS SP-75-2025 covers overall dimensions, tolerances, materials, chemical and tensile properties, heat treatment, notch-toughness, testing, marking and inspection for factory-made, seamless and electric-fusion-welded high-strength carbon and low-alloy steel buttwelding fittings in sizes NPS 2 through NPS 60 (DN 50 through DN 1500). The practice is written for high-pressure gas and oil transmission and distribution systems — pipelines, compressor stations, metering and regulating stations, and mains — governed by ASME B31.4 (liquid pipelines) and ASME B31.8 (gas transmission/distribution).
Fitting types covered: long-radius (LR) elbows, 3R elbows, straight and reducing tees, concentric and eccentric reducers, and caps. SP-75 does not tabulate short-radius (SR) elbows, short-radius returns, or 180° returns — those follow ASME B16.9 (with the former B16.28 SR content now merged into B16.9).
Edition referenced here: MSS SP-75-2025 (published June 2025, current).
Grades: WPHY 42, 46, 52, 56, 60, 65, 70.
Material specification: ASTM A860 / ASME SA-860.
Size rule: NPS 2–14 follow ASME B16.9 dimensions; NPS 16–60 use SP-75 own dimensional and tolerance tables.
2. WPHY Grade Overview — Mechanical Properties
| Grade |
Min Yield (MPa) |
Min Tensile (MPa) |
Min Elongation (%) |
Heat Treatment |
API 5L Equivalent |
| WPHY 42 |
290 |
415 |
25 |
Normalized (N) |
X42 |
| WPHY 46 |
317 |
434 |
25 |
Normalized (N) |
X46 |
| WPHY 52 |
359 |
455 |
25 |
Normalized (N) |
X52 |
| WPHY 56 |
386 |
490 |
20 |
Normalized (N) |
X56 |
| WPHY 60 |
414 |
517 |
20 |
Normalized (N) |
X60 |
| WPHY 65 |
448 |
531 |
20 |
QT |
X65 |
| WPHY 70 |
483 |
565 |
18 |
QT |
X70 |
3. Chemical Composition (Heat Analysis, Max %)
| Element |
Max, all WPHY grades |
| C |
0.30 |
| Mn |
1.60 |
| P |
0.035 |
| S |
0.035 |
| Si |
0.50 |
| Ni |
0.50 |
| Cr |
0.25 |
| Mo |
0.13 |
| V |
0.13 |
| Cb (Nb) |
0.10 |
| Ti |
0.05 |
| Cu |
0.50 |
Notes: Cu + Ni + Cr + Mo shall not exceed 1.00%. Carbon equivalent CE(IIW) = C + Mn/6 + (Cr + Mo + V)/5 + (Ni + Cu)/15 shall not exceed 0.45%. For WPHY 65/70 (QT) carbon is typically held ≤ 0.18% to satisfy toughness and sour-service limits.
4. Dimensional Letter Designations
Every dimension on this page uses the letter defined in the ASME/MSS fitting tables. The letters are fixed for each fitting type and are identical to ASME B16.9.
| Letter |
Applies to |
Definition |
| A |
90° elbows (LR & 3R) |
Centre-to-end distance (for a 90° elbow this equals the bend radius R) |
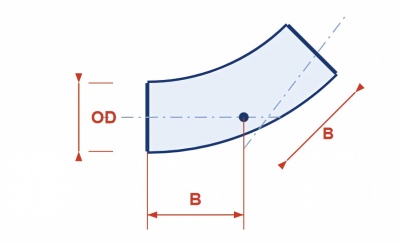
| B |
45° elbows (LR & 3R) |
Centre-to-end distance |
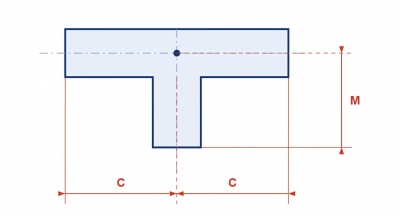
| C |
Tees and crosses |
Run centre-to-end |
| M |
Tees and crosses |
Outlet (branch) centre-to-end |
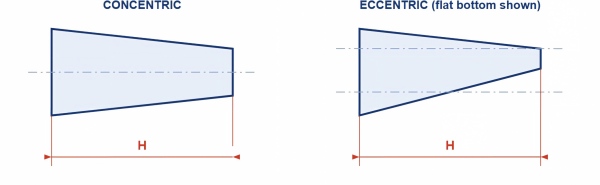
| H |
Reducers |
Overall length (end to end) |
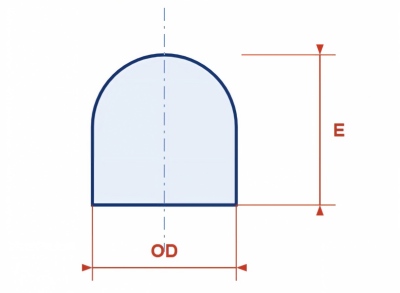
| E |
Caps |
Overall height (base to crown) |
| D |
All fittings |
Outside diameter at bevel (equals the matching pipe OD) |
5. 90° Elbows — Long Radius (LR, R = 1.5×NPS) and 3R (R = 3×NPS)
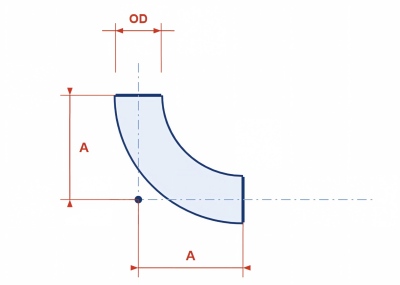
Long-radius values are identical to ASME B16.9 (A = 1.5 × NPS). The 3R elbow is unique to MSS SP-75: A = 3 × NPS. 3R elbows are tabulated from NPS 16; LR elbows run NPS 2–60.
| NPS |
DN |
LR 90° — A (mm) |
3R 90° — A (mm) |
| 2 |
50 |
76 |
152 |
| 2-1/2 |
65 |
95 |
190 |
| 3 |
80 |
114 |
229 |
| 3-1/2 |
90 |
133 |
267 |
| 4 |
100 |
152 |
305 |
| 5 |
125 |
190 |
381 |
| 6 |
150 |
229 |
457 |
| 8 |
200 |
305 |
610 |
| 10 |
250 |
381 |
762 |
| 12 |
300 |
457 |
914 |
| 14 |
350 |
533 |
— |
| 16 |
400 |
610 |
1220 |
| 18 |
450 |
686 |
1372 |
| 20 |
500 |
762 |
1524 |
| 22 |
550 |
838 |
1676 |
| 24 |
600 |
914 |
1829 |
| 26 |
650 |
991 |
1981 |
| 28 |
700 |
1067 |
2134 |
| 30 |
750 |
1143 |
2286 |
| 32 |
800 |
1219 |
2438 |
| 34 |
850 |
1295 |
2591 |
| 36 |
900 |
1372 |
2743 |
| 38 |
950 |
1448 |
2896 |
| 40 |
1000 |
1524 |
3048 |
| 42 |
1050 |
1600 |
3200 |
| 44 |
1100 |
1676 |
3353 |
| 46 |
1150 |
1753 |
3505 |
| 48 |
1200 |
1829 |
3658 |
| 50 |
1250 |
1905 |
3810 |
| 52 |
1300 |
1981 |
3962 |
| 54 |
1350 |
2057 |
4115 |
| 56 |
1400 |
2134 |
4267 |
| 58 |
1450 |
2210 |
4420 |
| 60 |
1500 |
2286 |
4572 |
LR 90° A = 38.1 × NPS (mm); 3R 90° A = 76.2 × NPS (mm) = 2 × LR A. NPS 16–60 3R values cross-checked against the MSS SP-75 3R elbow table (NPS 24 = 72 in = 1829 mm; NPS 60 = 180 in = 4572 mm).
6. 45° Elbows — Long Radius (LR) and 3R
LR 45° B = R × tan(22.5°) = 0.625 × NPS (inches) = 15.875 × NPS (mm), identical to ASME B16.9. 3R 45° B = 2 × LR B (R = 3×NPS).
| NPS |
DN |
LR 45° — B (mm) |
3R 45° — B (mm) |
| 2 |
50 |
32 |
64 |
| 2-1/2 |
65 |
40 |
79 |
| 3 |
80 |
48 |
95 |
| 3-1/2 |
90 |
56 |
111 |
| 4 |
100 |
64 |
127 |
| 5 |
125 |
79 |
159 |
| 6 |
150 |
95 |
190 |
| 8 |
200 |
127 |
254 |
| 10 |
250 |
159 |
318 |
| 12 |
300 |
190 |
381 |
| 14 |
350 |
222 |
— |
| 16 |
400 |
254 |
508 |
| 18 |
450 |
286 |
572 |
| 20 |
500 |
318 |
636 |
| 22 |
550 |
343 |
686 |
| 24 |
600 |
381 |
762 |
| 26 |
650 |
413 |
826 |
| 28 |
700 |
445 |
890 |
| 30 |
750 |
476 |
952 |
| 32 |
800 |
508 |
1016 |
| 34 |
850 |
540 |
1080 |
| 36 |
900 |
572 |
1144 |
| 38 |
950 |
603 |
1206 |
| 40 |
1000 |
635 |
1270 |
| 42 |
1050 |
667 |
1334 |
| 44 |
1100 |
699 |
1398 |
| 46 |
1150 |
730 |
1460 |
| 48 |
1200 |
762 |
1524 |
| 50 |
1250 |
794 |
1588 |
| 52 |
1300 |
826 |
1652 |
| 54 |
1350 |
857 |
1714 |
| 56 |
1400 |
889 |
1778 |
| 58 |
1450 |
921 |
1842 |
| 60 |
1500 |
953 |
1906 |
7. Tees and Crosses — Run (C) and Outlet (M)
For an equal tee C = M. Dimensions are identical to ASME B16.9. Reducer outlets take M from the outlet size.
| NPS |
DN |
C = M (mm) |
| 2 |
50 |
64 |
| 2-1/2 |
65 |
76 |
| 3 |
80 |
86 |
| 3-1/2 |
90 |
95 |
| 4 |
100 |
105 |
| 5 |
125 |
124 |
| 6 |
150 |
143 |
| 8 |
200 |
178 |
| 10 |
250 |
216 |
| 12 |
300 |
254 |
| 14 |
350 |
279 |
| 16 |
400 |
305 |
| 18 |
450 |
343 |
| 20 |
500 |
381 |
| 22 |
550 |
406 |
| 24 |
600 |
432 |
| 26 |
650 |
457 |
| 28 |
700 |
495 |
| 30 |
750 |
533 |
| 32 |
800 |
559 |
| 34 |
850 |
610 |
| 36 |
900 |
648 |
| 38 |
950 |
686 |
| 40 |
1000 |
724 |
| 42 |
1050 |
762 |
| 44 |
1100 |
800 |
| 46 |
1150 |
838 |
| 48 |
1200 |
876 |
| 50 |
1250 |
913 |
| 52 |
1300 |
949 |
| 54 |
1350 |
985 |
| 56 |
1400 |
1022 |
| 58 |
1450 |
1058 |
| 60 |
1500 |
1095 |
NPS 2–48 values are verbatim from ASME B16.9 (identical to SP-75). NPS 50–60 are the SP-75/B16.9 extended continuation; verify against the current SP-75-2025 tables for project-critical orders.
8. Reducers — Overall Length (H)
H is governed by the large end only. Concentric and eccentric reducers share the same H. Identical to ASME B16.9.
| Large end NPS |
DN |
H (mm) |
| 2 |
50 |
76 |
| 2-1/2 |
65 |
89 |
| 3 |
80 |
89 |
| 3-1/2 |
90 |
102 |
| 4 |
100 |
102 |
| 5 |
125 |
127 |
| 6 |
150 |
140 |
| 8 |
200 |
152 |
| 10 |
250 |
178 |
| 12 |
300 |
203 |
| 14 |
350 |
330 |
| 16 |
400 |
356 |
| 18 |
450 |
381 |
| 20 |
500 |
508 |
| 22 |
550 |
508 |
| 24 |
600 |
508 |
| 26 |
650 |
559 |
| 28 |
700 |
610 |
| 30 |
750 |
660 |
| 32 |
800 |
711 |
| 34 |
850 |
762 |
| 36 |
900 |
813 |
| 38 |
950 |
864 |
| 40 |
1000 |
914 |
| 42 |
1050 |
965 |
| 44 |
1100 |
1016 |
| 46 |
1150 |
1067 |
| 48 |
1200 |
1118 |
| 50 |
1250 |
1165 |
| 52 |
1300 |
1212 |
| 54 |
1350 |
1258 |
| 56 |
1400 |
1305 |
| 58 |
1450 |
1351 |
| 60 |
1500 |
1398 |
NPS 2–48 verbatim from ASME B16.9; NPS 50–60 per SP-75/B16.9 extended continuation (verify against current standard).
9. Caps — Overall Height (E)
E is the only dimensional envelope SP-75 fixes for a cap, identical to ASME B16.9. The crown profile (ellipsoidal or hemispherical) is left to the manufacturer.
| NPS |
DN |
E (mm) |
| 2 |
50 |
38 |
| 2-1/2 |
65 |
38 |
| 3 |
80 |
51 |
| 3-1/2 |
90 |
64 |
| 4 |
100 |
64 |
| 5 |
125 |
76 |
| 6 |
150 |
89 |
| 8 |
200 |
102 |
| 10 |
250 |
127 |
| 12 |
300 |
152 |
| 14 |
350 |
165 |
| 16 |
400 |
178 |
| 18 |
450 |
203 |
| 20 |
500 |
229 |
| 22 |
550 |
254 |
| 24 |
600 |
267 |
| 26 |
650 |
267 |
| 28 |
700 |
267 |
| 30 |
750 |
267 |
| 32 |
800 |
267 |
| 34 |
850 |
267 |
| 36 |
900 |
267 |
| 38 |
950 |
305 |
| 40 |
1000 |
305 |
| 42 |
1050 |
305 |
| 44 |
1100 |
343 |
| 46 |
1150 |
343 |
| 48 |
1200 |
343 |
| 50 |
1250 |
343 |
| 52 |
1300 |
343 |
| 54 |
1350 |
343 |
| 56 |
1400 |
343 |
| 58 |
1450 |
343 |
| 60 |
1500 |
343 |
Cap height E plateaus above NPS 38 (305 mm) then 44 (343 mm) and holds through NPS 60 per SP-75/B16.9 continuation.
10. 180° Returns and Short-Radius Fittings — Not Covered by SP-75
MSS SP-75 tabulates only long-radius (1.5D) and 3R (3D) elbows, tees, reducers and caps. It does not publish dimensions for 180° returns or short-radius (1D) fittings. Those items follow ASME B16.9 (which since 2024-08-31 also contains the former ASME B16.28 short-radius content). When a pipeline project needs a 180° return or an SR elbow in WPHY material, specify the geometry per B16.9 and the material/heat-treatment package per SP-75 on the purchase order.
11. Heat Treatment Requirements
| Grade |
Required Heat Treatment |
Typical Process Temperature |
| WPHY 42 |
Normalized (N) |
900–960°C, air cooled |
| WPHY 46 |
Normalized (N) |
900–960°C, air cooled |
| WPHY 52 |
Normalized (N) |
900–960°C, air cooled |
| WPHY 56 |
Normalized (N) |
900–960°C, air cooled |
| WPHY 60 |
Normalized (N) |
900–960°C, air cooled |
| WPHY 65 |
Quenched and Tempered (QT) |
900–940°C water quench + 550–650°C temper |
| WPHY 70 |
Quenched and Tempered (QT) |
900–940°C water quench + 550–650°C temper |
12. Mechanical Testing Requirements
| Test |
Requirement |
| Tensile test (body) |
Yield, tensile, elongation — per grade table above |
| Bend test |
Free-bend to 180° without cracking for WPHY 42–52; guided-bend for higher grades |
| Charpy V-notch impact |
Min avg 20 J (15 ft·lbf) at design temp; individual ≥ 16 J (12 ft·lbf) |
| Hydrostatic test |
1.5× minimum allowable pressure from B31.4 or B31.8 hoop-stress formula |
| Wall thickness UT |
Mandatory for WPHY 65/70; recommended for WPHY 42–60 |
| PMI (Positive Material ID) |
Strongly recommended; confirms chemistry compliance |
13. Tolerances (per MSS SP-75, NPS 16–60)
Tolerances are equal plus and minus unless noted. For NPS 2–14 the ASME B16.9 tolerance tables apply (identical dimensions).
| Dimension |
NPS 16 – 24 |
NPS 26 – 36 |
NPS 38 – 48 |
NPS 50 – 60 |
| Centre-to-end A, B, C, M (LR) |
±2.3 |
±3.0 |
±4.8 |
per SP-75 extended |
| 3R elbow centre-to-end |
2.5% of the dimension |
2.5% of the dimension |
| Overall length of reducers, H |
±3.0 |
±6.4 |
±9.7 |
per SP-75 extended |
| Overall height of caps, E |
±2.3 |
±4.8 |
±9.7 |
per SP-75 extended |
| Outside diameter at bevel, D |
Per ASME B16.9 OD tolerances for the matching pipe size |
14. Marking Requirements
| Marking element |
Example |
| Manufacturer name or trademark |
HT PIPE |
| Material designation |
WPHY 60 (per ASTM A860 / ASME SA-860) |
| Nominal size |
NPS 24 |
| Schedule or wall thickness |
Per API 5L X60 pipe wall |
| Compliance marking |
MSS SP-75 |
| Heat number / batch traceability |
Heat No. / Batch No. |
15. MSS SP-75 vs ASME B16.9 vs ASME B16.28 — Comparison
| Parameter |
MSS SP-75 |
ASME B16.9 |
ASME B16.28 |
| Size range |
NPS 2–60 (NPS ≤14 per B16.9; 16–60 own tables) |
NPS 1/2–48 |
NPS 1/2–24 (SR, withdrawn) |
| Yield strength |
290–565 MPa (WPHY 42–70) |
240 MPa (WPB) |
240 MPa (WPB) |
| Centre-to-end dimensions |
Same as B16.9; adds 3R elbows |
B16.9 tables (LR/SR) |
B16.9 tables (SR only) |
| Fitting weight |
Geometrically identical to B16.9; lighter possible only via thinner wall (higher yield) |
Standard |
SR — compact |
| Heat treatment |
N or QT mandatory |
Per SA-234 (WPB annealed) |
Per SA-234 |
| Charpy CVN required |
Yes — mandatory |
No mandatory CVN |
No mandatory CVN |
| Application code |
B31.4 / B31.8 |
B31.3 |
B31.3 |
16. Related Standards
| Standard |
Title |
| ASTM A860 / ASME SA-860 |
Wrought High-Strength Carbon and Low-Alloy Steel Fittings (material specification for SP-75) |
| API 5L |
Line Pipe (X42–X80, matching pipe grades for SP-75 fittings) |
| ASME B31.4 |
Pipeline Transportation Systems for Liquids |
| ASME B31.8 |
Gas Transmission and Distribution Piping Systems |
| ASME B16.9 |
Factory-Made Wrought Buttwelding Fittings (dimensions for NPS ≤ 14; also SR/returns) |
| ASME B16.25 |
Buttwelding Ends |
| MSS SP-25 |
Standard Marking System for Valves, Fittings, Flanges and Unions |
17. How to Order (Per MSS SP-75)
| Order Element |
Specification |
Example |
| Standard |
MSS SP-75 |
SP-75 |
| Fitting type |
Elbow / Tee / Reducer / Cap (LR or 3R) |
LR 90° Elbow |
| Size |
NPS |
24 |
| WPHY grade |
WPHY 42 / 46 / 52 / 56 / 60 / 65 / 70 |
WPHY 60 |
| Wall thickness / Schedule |
Per project pipeline spec |
Per API 5L X60 pipe wall |
| Ends |
Beveled per B16.25 |
Beveled |
| Charpy test temperature |
Design temperature (e.g. –30°C) |
–30°C, 20 J avg |
| NDE requirements |
UT, MPI, RT per code |
100% UT body wall |
| Material test report |
EN 10204 3.1 MTC |
3.1 MTC + CVN results |
18. FAQ — Frequently Asked Questions
What is the maximum size of MSS SP-75 fittings?
MSS SP-75-2025 covers fittings NPS 2 through NPS 60 (DN 50 through DN 1500). This is larger than ASME B16.9, which stops at NPS 48. Fittings NPS 2–14 follow ASME B16.9 dimensions; NPS 16–60 are governed by SP-75 own dimensional and tolerance tables. The seamless (weld-free) manufacturing limit of many mills is NPS 24, but the standard itself permits welded and electric-fusion-welded construction up to NPS 60.
Are MSS SP-75 fittings dimensionally the same as ASME B16.9?
Yes — the geometry is identical. MSS SP-75 uses the same centre-to-end (A, B, C, M) and end-to-end (E, H) dimensions as ASME B16.9. A 24 in long-radius elbow has the same shape whether made to SP-75 or B16.9 (A = 914 mm for both). SP-75 adds 3R long-radius elbows (R = 3 × NPS, e.g. 4572 mm / 180 in for NPS 60) that ASME B16.9 does not list, and applies its own tolerance tables for NPS 16–60. Because the material, heat treatment and impact testing differ, the purchase order must still call out SP-75 for pipeline-grade fittings even though the dimensions match B16.9.
What is the difference between WPHY and WPB fittings?
WPHY (Wrought Pipe High-Yield) fittings per MSS SP-75 are made from high-strength normalized or quenched-and-tempered carbon-manganese steels with yield strengths from 290 MPa (WPHY 42) to 565 MPa (WPHY 70) — well above WPB (240 MPa yield per ASTM A234 / SA-234). This allows thinner-walled, lighter pipeline systems at higher pressure. WPHY fittings serve ASME B31.4 (liquid pipelines) and B31.8 (gas pipelines); WPB fittings serve ASME B31.3 (process piping). The two share the same centre-to-end dimensions — the difference is material grade, mandatory heat treatment and Charpy testing, not geometry.
What heat treatment is required for WPHY fittings?
WPHY 42 through WPHY 60 are typically supplied normalized (N). WPHY 65 and WPHY 70 are typically supplied quenched and tempered (QT) to reach the higher yield strength. Normalizing heats to 900–960°C and air-cools; QT austenitizes at 900–940°C, water-quenches, then tempers at 550–650°C. PWHT is generally not required for WPHY fittings in pipeline service unless the surrounding components or code require it.
Why is Charpy V-notch impact testing mandatory for SP-75 fittings?
Pipeline fittings undergo heavy plastic deformation during forming (elbows are bent, tees are extruded), which can reduce notch toughness — especially at the heavily worked extrados of an elbow. MSS SP-75 requires Charpy V-notch (CVN) impact testing for all WPHY grades: minimum average absorbed energy 20 J (15 ft·lbf) at the design temperature, with no individual value below 16 J (12 ft·lbf). For Arctic or sub-zero service the test temperature must match or be lower than the design temperature. CVN testing confirms the fitting retains toughness after forming and heat treatment.