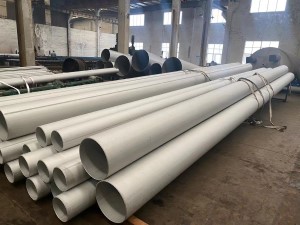
General Fluid Service Pipe, Black or Hot-Dip Galvanised
|
GRADE
A53 Gr B
|
TYPES
S / E / F
|
PRODUCT FORM
Pipe, black or galvanised
|
UTS (MIN)
415 MPa
|
YIELD (MIN)
240 MPa
|
SERVICE
General fluid
|
|
ASTM A53 is the general-purpose carbon steel pipe specification. One standard covers seamless, electric-resistance-welded and furnace-welded pipe, black or hot-dip galvanised, in sizes from NPS 1/8 to NPS 26. It is the pipe most often specified for water, air, steam at moderate temperature, and structural applications.
|
|
C
≤0.30%
Strength and weldability
|
Mn
≤1.20%
Strength; higher than A106 allows
|
P + S
0.05 / 0.045%
Looser than A106
|
Cu + Ni + Cr + Mo + V
≤1.00%
Residual sum limit
|
|
UTS
≥415 MPa
|
YS 0.2%
≥240 MPa
|
Elong.
Per A53 equation
|
Types
S / E / F
|
What is ASTM A53?
A53 comes in three manufacturing types. Type S is seamless, Type E is electric-resistance welded, and Type F is furnace butt welded, now limited in size and rarely ordered. Grade B is the common grade, with Grade A used for lower pressure work. Chemistry is deliberately looser than A106: manganese is allowed up to 1.20% against 1.06%, sulfur to 0.045% against 0.035%, and there is no silicon minimum.
That looser chemistry has a consequence. Without a silicon minimum the steel is not necessarily fully killed, and the specification is therefore limited to general fluid service rather than high temperature pressure service. ASME B31.3 lists A53 only to about 204°C, while A106 goes to 538°C. For a steam line at 300°C the two are not interchangeable, even though the tensile and yield minima are identical.
Galvanising is one of the reasons A53 remains so widely used. Hot-dip coating to ASTM A90 gives atmospheric corrosion protection for water, fire protection and outdoor structural piping at a cost that stainless cannot approach. The coating is not a substitute for a corrosion allowance in aggressive media, and the threads are cut after galvanising or protected during coating.
Chemical Composition (Weight %)
A53 chemical requirements, Grade B. The values are maxima unless shown otherwise, and Type F carries slightly different limits for Grade A.
| Element |
Min (%) |
Max (%) |
Role in Alloy |
| Carbon (C) |
— |
0.30 |
Strength; 0.25 for Grade A |
| Manganese (Mn) |
— |
1.20 |
Strength and deoxidation |
| Phosphorus (P) |
— |
0.05 |
Impurity; looser than A106 |
| Sulfur (S) |
— |
0.045 |
Impurity; looser than A106 |
| Copper (Cu) |
— |
0.40 |
Residual; 0.20 min when copper-bearing is ordered |
| Nickel (Ni) |
— |
0.40 |
Residual |
| Chromium (Cr) |
— |
0.40 |
Residual |
| Molybdenum (Mo) |
— |
0.15 |
Residual |
| Vanadium (V) |
— |
0.08 |
Residual |
The sum of Cu + Ni + Cr + Mo + V is limited to 1.00%. For each 0.01% of carbon below the maximum, manganese may be raised by 0.06% above the stated limit, to 1.35% for Type S and 1.65% for Type E.
Mechanical Properties
A53 tensile requirements. Elongation is not a fixed number in this standard; it is calculated from the specimen area and the specified tensile strength.
| Condition / Specimen |
UTS (MPa) |
YS 0.2% (MPa) |
Elong. % min |
Hardness |
| Grade A, minimum |
≥330 |
≥205 |
Per equation |
Not specified |
| Grade B, minimum |
≥415 |
≥240 |
Per equation |
Not specified |
| Grade B Type S, typical |
450-560 |
260-340 |
28-36 |
120-170 HBW |
| Grade B Type E, typical |
430-540 |
250-330 |
25-33 |
120-170 HBW |
The minimum elongation in 50 mm is calculated from e = 625000 A0.2 / U0.9, where A is the lesser of 500 mm² and the specimen cross-section, and U the specified minimum tensile strength. For standard wall Grade B this lands at about 30%; thin-wall or small specimens can require more. Quoting a single percentage for A53 is therefore always an approximation.
Physical Properties
| Property |
Value |
Note |
| Density |
7.85 g/cm³ |
At 20°C |
| Melting Range |
1425-1540°C |
Solidus approximately 1425°C |
| Thermal Conductivity |
51 W/m·K |
At 100°C |
| Thermal Expansion |
11.7 ×10⁻⁶ /K |
20-100°C |
| Specific Heat |
486 J/kg·K |
At 20°C |
| Electrical Resistivity |
0.16 µΩ·m |
At 20°C |
| Modulus of Elasticity |
200 GPa |
About 185 GPa at 400°C |
Zinc coating adds roughly 0.06 kg/m² per 10 µm of thickness. A standard A90 coating on 2-inch pipe weighs about 0.49 kg/m, which matters for support spacing and for handling.
| HEAT TREATMENT & FABRICATION |
|
Heat Treatment, Welding & PWHT
Supply condition
A53 pipe is supplied as manufactured, with no mandatory heat treatment. Electric-resistance welded pipe above NPS 4 may be ordered with the weld seam heat treated, and Type E pipe is normally supplied with the weld normalised in line. Cold drawn pipe is stress relieved.
Galvanising
Hot-dip coating to ASTM A90 is applied after forming. Threads are either cut before coating and chased afterwards, or cut after galvanising and coated with zinc-rich paint. Cut threads expose bare steel and are the first area to corrode on a galvanised line.
Welding
Galvanised pipe can be welded, but the zinc coating must be removed for at least 25 mm either side of the joint and the fumes extracted. Zinc oxide fume causes metal fume fever; ventilation is a health requirement, not a comfort measure. ER70S-6 is suitable for both black and stripped galvanised pipe.
Post-weld heat treatment
Not normally required. P-No. 1 rules apply as for A106, but most A53 service is thin-wall and low temperature, so PWHT rarely arises.
Service Limits & Corrosion Behaviour
Temperature envelope
ASME B31.3 lists A53 to about 204°C. Above that, the absence of a silicon minimum and the looser sulfur limit make A106 the correct specification. In fire protection and water service the temperature is not the governing condition at all.
Corrosion and coating life
Black pipe corrodes at a rate set by the environment, roughly 0.05-0.1 mm/year in clean water and much faster in chlorides. Galvanised pipe gives 15-30 years in rural and urban atmospheres, less in marine or industrial conditions. Coating life is proportional to thickness, which is why coating mass is specified rather than coating presence.
Pressure rating
Wall thickness is selected from ASME B36.10 schedules, and pressure rating follows B31.1 or B31.3 allowable stress. Schedule 40 is the default for general service, Schedule 80 where mechanical damage or higher pressure is expected.
Low temperature
A53 has no impact requirement and is not a low temperature material. Below -29°C, A333 Grade 6 is the correct specification.
ASTM A53 vs Similar Grades — Selection Guide
| If you need... |
Choose... |
Why |
| General water, air, low-pressure service |
A53 Gr B |
Lowest cost, widely available |
| High temperature above 204°C |
A106 Gr B |
Silicon-killed, listed to 538°C |
| Outdoor or buried water line |
A53 galvanised |
Zinc coating, no painting needed |
| Fire protection |
A53 Gr B, UL/FM |
Listed pipe with approval |
| Low temperature |
A333 Gr 6 |
Impact tested to -46°C |
| Precision or high pressure |
A106 / API 5L |
Tighter chemistry and tolerances |
A53 Type S is not simply a cheaper A106. Without killed-steel practice and with a higher sulfur allowance, it is a different product with a narrower temperature envelope, and substituting it in a steam line is a common and avoidable error.
Applicable Standards
| Standard |
Scope |
| ASTM A53 / A53M |
Pipe, steel, black and hot-dipped, zinc-coated, welded and seamless |
| ASTM A90 |
Weight of coating on zinc-coated iron and steel articles |
| ASME B36.10M |
Welded and seamless wrought steel pipe dimensions |
| ASME B1.20.1 |
Pipe threads, general purpose |
| ASME B31.3 |
Process piping: allowable stress and temperature limit |
| ASTM A700 |
Packaging, marking and loading practices |
HT PIPE Supply — ASTM A53 Product Forms
| Product Form |
Specification |
HT PIPE Supply |
| Seamless pipe, Sch 40 / 80 |
A53 Gr B Type S, B36.10 |
In stock, NPS 1/8-16 |
| ERW pipe, Sch 10 - 80 |
A53 Gr B Type E, B36.10 |
In stock, NPS 1/2-24 |
| Galvanised pipe, threaded and coupled |
A53 Gr B, ASTM A90 coating |
In stock, NPS 1/2-8 |
| Plain end and bevelled |
A53 Gr B, B36.10 |
Available |
| Large diameter ERW |
A53 Gr B Type E, to 26 in |
On order |
| Matching fittings |
A234 WPB / malleable iron |
Available |
Galvanised pipe is supplied with coating mass test results to A90 and thread inspection to B1.20.1. Mill test certificates to EN 10204 3.1 accompany every heat.
Project Experience — ASTM A53
A53 pipe is supplied for water transmission, fire protection, compressed air and general industrial service, in black and galvanised finishes.
| Project |
Product |
Specification |
| Municipal water network (Middle East) |
A53 Gr B, Sch 40, galvanised |
A53, B36.10 |
| Fire protection system (Southeast Asia) |
A53 Gr B, Sch 40, red painted |
A53, B36.10 |
| Compressed air ring main (China) |
A53 Gr B, Sch 80, black |
A53, B36.10 |
For galvanised orders we confirm coating mass, thread type and end finish before production, because these details decide whether the pipe can be installed without rework.
| FREQUENTLY ASKED QUESTIONS |
|
FAQ — ASTM A53
| What is the difference between A53 and A106? |
| A106 requires a silicon minimum of 0.10% and tighter sulfur, and is listed to 538°C. A53 has no silicon requirement, allows more sulfur and manganese, and is limited to about 204°C in B31.3. Strength minima are the same, which is why they get confused. |
| What are Type S, E and F in A53? |
| Type S is seamless, Type E is electric-resistance welded, and Type F is furnace butt welded. Type F is limited in size and rarely ordered today. Type E dominates the market in sizes up to 24 inch. |
| Is A53 pipe suitable for potable water? |
| Galvanised A53 is used for potable water, but the zinc coating can raise zinc and lead levels in soft water, and many utilities now specify cement-lined or plastic pipe instead. Check the local authority requirement before ordering. |
| Why is elongation not a fixed percentage in A53? |
| Because A53 calculates the minimum from specimen area and tensile strength. Small or thin-wall specimens require higher elongation, so a single figure cannot apply to every size. The mill certificate shows the calculated value for the specimen tested. |
| Can galvanised A53 pipe be welded? |
| Yes, after removing the zinc coating at least 25 mm from the joint and providing fume extraction. Welding through the coating produces porosity and toxic zinc fume, and leaves a joint that corrodes faster than the surrounding pipe. |
|
Need ASTM A53 for Your Project?
HT PIPE supplies A53 Grade B pipe in seamless, ERW and galvanised finishes, with A90 coating results and B1.20.1 thread inspection. Send the size schedule and end finish for a quotation.
Request a Quote |
|
MATERIAL PAGE
|
MATERIAL PAGE
|
MATERIAL PAGE
|
PRODUCT PAGE
|