Chromium-Molybdenum Fittings for Refinery and Steam Service Above the Carbon Steel Range
|
GRADE
A234 WP11
|
UNS
K11597
|
FAMILY
1¼Cr-½Mo
|
UTS
415-585 MPa
|
YIELD (MIN)
205 MPa
|
CODE RANGE
-29 to 649°C
|
|
ASTM A234 WP11 is the 1¼Cr-½Mo wrought fitting grade. The chromium addition lifts oxidation resistance and the molybdenum raises creep strength, so WP11 holds its allowable stress where plain carbon steel has already dropped off, roughly from 430°C upward. It is the first step on the chrome-moly ladder above A234 WPB.
|
|
Cr
1.00-1.50%
Oxidation, creep strength
|
Mo
0.44-0.65%
Creep resistance
|
C
0.05-0.15%
Carbide former
|
Si
0.50-1.00%
Oxidation resistance
|
|
UTS
415-585 MPa
|
YS 0.2%
≥205 MPa
|
Elong.
≥20%
|
Service
-29~593°C
|
What is ASTM A234 WP11?
WP11 is a ferritic low-alloy steel with 1.00-1.50% chromium and 0.44-0.65% molybdenum. Carbon is held to 0.05-0.15%, which is deliberately narrower than WPB on both ends: enough carbon to form the carbides that carry creep load, not so much that toughness or weldability suffers. Silicon runs 0.50-1.00% for oxidation resistance.
The grade is common in refinery hydrotreating, catalytic reforming, and high-pressure steam piping, and in heat recovery steam generators where the design temperature sits between the carbon steel and 2¼Cr limits. Fittings are hot formed and then normalised and tempered, so the microstructure is ferrite with spheroidised carbides rather than the banded as-rolled structure of carbon steel.
WP11 is not a substitute for WP22 on creep grounds. Above about 540°C in steam service, or where hydrogen partial pressure is high, 2¼Cr-1Mo or 9Cr-1Mo-V is the correct choice. The two grades are visually similar after sandblasting, so PMI on every fitting is standard practice on refinery turnarounds.
Chemical Composition (Weight %)
A234 chemical requirements for WP11. Phosphorus and sulfur are capped at 0.030% each, tighter than the carbon grades because the fitting will run hot for decades and residuals govern temper embrittlement.
| Element |
Min (%) |
Max (%) |
Role in Alloy |
| Carbon (C) |
0.05 |
0.15 |
Carbide formation; both limits are functional, not nominal |
| Manganese (Mn) |
0.30 |
0.60 |
Strength; kept low to protect toughness |
| Phosphorus (P) |
— |
0.030 |
Impurity; drives temper embrittlement |
| Sulfur (S) |
— |
0.030 |
Impurity; controls inclusion shape and toughness |
| Silicon (Si) |
0.50 |
1.00 |
Oxidation resistance |
| Chromium (Cr) |
1.00 |
1.50 |
Oxidation and creep strength |
| Molybdenum (Mo) |
0.44 |
0.65 |
Creep strength; raises high-temperature strength |
| Nickel (Ni) |
— |
0.40 |
Residual |
| Copper (Cu) |
— |
0.40 |
Residual |
A234 applies a residual sum limit of Cu + Ni + Cr + Mo ≤ 1.00% to the carbon grades; for WP11 the chromium and molybdenum are intentional, so the requirement is read as a cap on the residual elements only. Product analysis tolerances of A960 apply.
Mechanical Properties
Tensile requirements of A234 for WP11, in the normalised and tempered condition in which the fittings are supplied.
| Condition / Specimen |
UTS (MPa) |
YS 0.2% (MPa) |
Elong. % min |
Hardness |
| Minimum, A234 Table 2 |
415-585 |
205 |
20 |
Not mandated |
| Typical normalised + tempered |
470-540 |
250-320 |
24-30 |
135-170 HBW |
| Long-term service, aged |
460-530 |
260-330 |
22-28 |
140-175 HBW |
The 585 MPa upper limit matters: heats that test harder than the range are rejected even though the yield is acceptable, because excess strength in a Cr-Mo fitting usually means an incomplete temper. Hardness is not mandated by A234 for WP11, but 190 HBW is a common purchase-order ceiling and 22 HRC applies where NACE MR0175 is invoked.
Physical Properties
| Property |
Value |
Note |
| Density |
7.85 g/cm³ |
At 20°C |
| Melting Range |
1430-1510°C |
Solidus approximately 1430°C |
| Thermal Conductivity |
42 W/m·K |
At 100°C; 36 W/m·K at 400°C |
| Thermal Expansion |
12.4 ×10⁻⁶ /K |
20-100°C |
| Specific Heat |
470 J/kg·K |
At 20°C |
| Electrical Resistivity |
0.25 µΩ·m |
At 20°C |
| Modulus of Elasticity |
205 GPa |
About 185 GPa at 450°C |
Thermal expansion is higher than carbon steel, which matters at dissimilar joints to A106 pipe: the weld sees an expansion mismatch of about 7% at 500°C, and that is one reason PWHT and a tapered transition are specified.
| HEAT TREATMENT & FABRICATION |
|
Heat Treatment, Welding & PWHT
Normalising and tempering
A234 requires heat treatment for WP11. The fitting is normalised at 900-960°C, air cooled, then tempered at 650-730°C. Normalising from the wrong temperature leaves delta ferrite or coarse grains, and a temper below 650°C leaves hardness above the range. Both show up on the mill certificate, so read the cycle, not just the result.
Post-weld heat treatment
B31.3 classifies WP11 as P-No. 4. PWHT is mandatory for all thicknesses in most specifications and runs at 704-760°C, with a minimum hold of one hour per 25 mm. Cooling below 315°C should be controlled. Skipping PWHT leaves a hard, brittle heat-affected zone that will crack in thermal cycling.
Welding
Preheat at 150-200°C and maintain interpass below 300°C. Filler metal is ER80S-B2 for GTAW and E8018-B2 for SMAW, matched to the 1¼Cr-½Mo deposit. Do not use carbon steel filler: the joint then has a soft, low-creep-strength band that becomes the life-limiting detail of the line.
Dissimilar joints
When WP11 meets A106 Gr B, the joint is usually buttered or made with ER80S-B2 and PWHT is governed by the Cr-Mo side. The transition is placed where the design temperature is lowest, and the weld is examined by radiography after PWHT, not before.
Service Limits & Corrosion Behaviour
Temperature envelope
ASME B31.3 Table A-1 lists A234 WP11 to 649°C. In practice the grade is specified for steam and hydrocarbon service to about 540°C; above that, creep rupture data favour WP22. Between 540 and 593°C the choice depends on wall thickness and design life, not on the code ceiling.
Oxidation and scaling
The 1.25% chromium raises resistance to steam oxidation compared with carbon steel. Scaling becomes significant above about 565°C, which is one reason not to run WP11 at the top of its code range in steam.
Hydrogen service
WP11 appears on the Nelson curves for hydrotreating and hydrodesulfurisation. The allowable hydrogen partial pressure falls as temperature rises; the curve, not the fitting standard, sets the grade. Above the WP11 line the specification moves to WP22 or WP91.
Temper embrittlement
The 1¼Cr grade is less sensitive than 2¼Cr, but long service in the 370-565°C band still embrittles the steel. Impact testing after step cooling is available on request for critical service, and weld repair of aged fittings should be approached with care.
ASTM A234 WP11 vs Similar Grades — Selection Guide
| If you need... |
Choose... |
Why |
| Up to 427°C, non-corrosive |
WPB |
Lower cost, no heat treatment |
| 430-540°C steam or hydrocarbon |
WP11 |
Creep strength at moderate alloy cost |
| 540-600°C, high hydrogen partial pressure |
WP22 |
Higher Cr and Mo, better creep life |
| Above 600°C or thermal cycling |
WP91 |
9Cr-1Mo-V, much higher creep strength |
| Wet H₂S service |
WP11 with hardness control |
NACE MR0175, 22 HRC ceiling |
| Low temperature |
A420 WPL6 / stainless |
WP11 is not tough below -29°C |
WP11 and WP22 are often confused at the receiving inspection because both are chrome-moly. Positive material identification with an alloy analyser is the only reliable field check; hardness alone will not separate them.
Applicable Standards
| Standard |
Scope |
| ASTM A234 / A234M |
Wrought carbon and alloy steel fittings, WP11 grade |
| ASME B16.9 |
Factory-made wrought butt-welding fittings |
| ASME B16.28 |
Short-radius elbows and return bends |
| ASME B16.25 |
Butt-welding ends |
| ASTM A960 |
Common requirements for wrought fittings |
| ASTM A182 F11 |
Matching forged flanges and forged fittings |
| ASME B31.3 |
Process piping: P-No. 4 PWHT requirements |
HT PIPE Supply — ASTM A234 WP11 Product Forms
Each heat is supplied with the normalising and tempering cycle on the certificate, hardness results, and Charpy data where specified. PMI is performed on 100% of fittings for refinery orders.
Project Experience — ASTM A234 WP11
WP11 fittings are supplied into hydrotreating, steam and HRSG service where the design temperature sits just above the carbon steel range.
| Project |
Product |
Specification |
| Diesel hydrotreater (Middle East) |
WP11 elbows and tees, Sch 80 |
A234 WP11, B16.9 |
| HRSG high-pressure steam (Southeast Asia) |
WP11 reducers and caps |
A234 WP11, B16.9 |
| Reformer unit piping (China) |
WP11 fittings, PWHT |
A234 WP11, B16.9 |
Our team reviews the design temperature, hydrogen partial pressure and PWHT window before confirming the grade, because the fitting standard alone does not answer those questions.
| FREQUENTLY ASKED QUESTIONS |
|
FAQ — ASTM A234 WP11
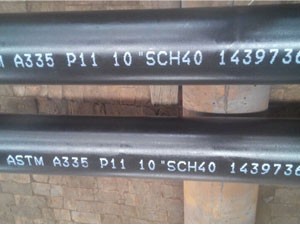
| Is A234 WP11 the same as A335 P11? |
| No. A335 P11 covers seamless pipe and A234 WP11 covers wrought fittings. They share the same chemistry and strength requirements, which is why they are welded together, but the dimensional, testing and marking requirements come from different standards. |
| Does WP11 have to be heat treated? |
| Yes. A234 requires the Cr-Mo grades to be heat treated. The normal cycle is normalise at 900-960°C, air cool, then temper at 650-730°C. A fitting supplied as-formed is non-compliant regardless of what the mechanical test shows. |
| What is the PWHT temperature for WP11? |
| 704-760°C under ASME B31.3 for P-No. 4 material, with a hold of one hour per 25 mm of thickness and a one hour minimum. Heating and cooling above 315°C should be controlled to avoid thermal gradients across the fitting. |
| Can WP11 be welded to carbon steel? |
| Yes, and it is common at battery limits. Use an ER80S-B2 or E8018-B2 deposit, preheat at 150-200°C, and PWHT to the Cr-Mo side requirement. The joint is then examined after heat treatment. |
| Why does the specification cap tensile strength at 585 MPa? |
| Because a higher reading usually means the temper was incomplete or the chemistry is off. In Cr-Mo steel, excess strength is a symptom of a microstructure that will embrittle in service, so A234 sets both a floor and a ceiling. |
|
Need ASTM A234 WP11 for Your Project?
HT PIPE supplies A234 WP11 fittings with normalising and tempering cycles documented, hardness and Charpy results, and PMI on request. Send the design temperature and line class and we will confirm grade and PWHT parameters.
Request a Quote |
|
MATERIAL PAGE
|
MATERIAL PAGE
|
MATERIAL PAGE
|
PRODUCT PAGE
|